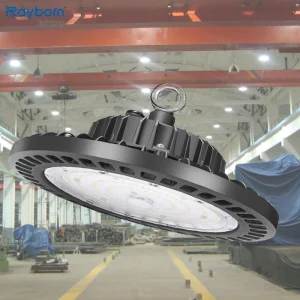
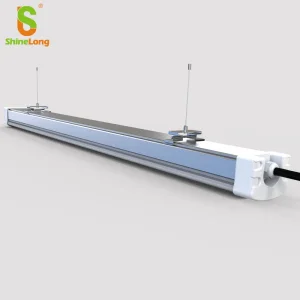
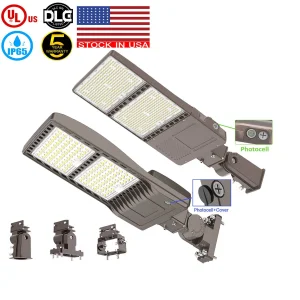
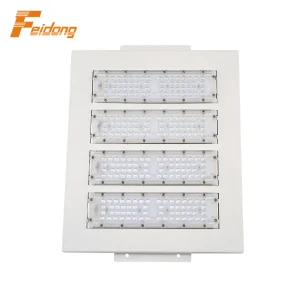
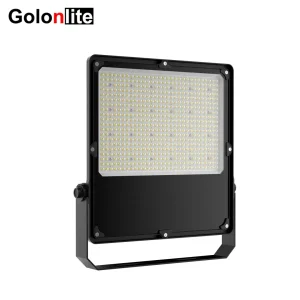
Shanghai Lume Light Co., Ltd. has grown into a reliable LED lighting manufacturer, specializing in industrial, area, and garden lighting solutions for global markets. Since its establishment, the company has focused on delivering energy-efficient, durable, and high-performance lighting products that meet the evolving needs of commercial and industrial applications.
Based in Shanghai, a major international business and technology center, Lume Light benefits from strong supply chain resources and advanced manufacturing capabilities. The company operates a modern production facility equipped with automated assembly lines and strict quality control systems, ensuring consistent product performance and reliability.
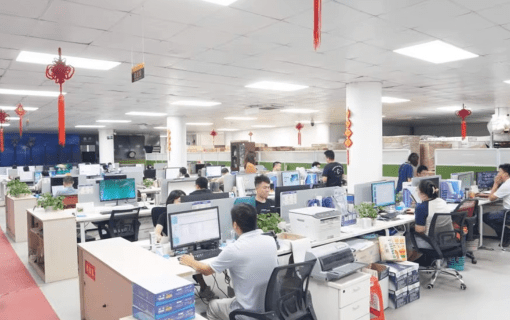
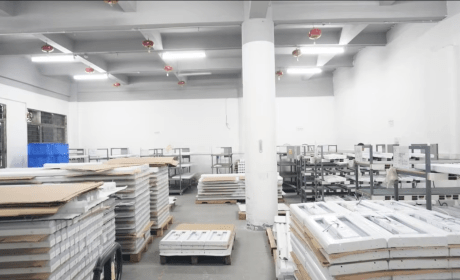
Over the years, Shanghai Lume Light has expanded its product portfolio to include industrial lighting systems for factories and warehouses, high-efficiency area lighting for large outdoor spaces, and decorative yet functional garden lighting solutions. Its products are widely used in infrastructure projects, commercial complexes, and landscape lighting applications.
Driven by innovation and sustainability, the company continues to invest in research and development, integrating smart lighting technologies and energy-saving designs. With a commitment to quality and customer satisfaction, Shanghai Lume Light Co., Ltd. is steadily strengthening its global presence and providing efficient, future-ready LED lighting solutions worldwide.
Global industrial facilities face stringent carbon reduction regulations. Upgrading to high-lumen OEM LED work lights and industrial luminaires is no longer optional—it is a core component of corporate ESG compliance and operational cost optimization.
Modern manufacturing plants, oil and gas sectors, and large logistic warehouses demand lighting fixtures with high IP ratings (IP65/IP66), IK impact resistance, and corrosion-proof aluminum housings to endure extreme operational stressors.
The transition toward smart factories accelerates the demand for radar microwave motion sensors, IoT-connected dimming systems, and power/CCT switchable LED fixtures that dynamically adapt to real-time spatial requirements.
Rigorous aging and waterproof testing prior to dispatch.
Backed by premium drivers and robust thermal management.
Tailored lumen output, branding, and optical distribution.
CE, CB, ENEC, UL, and RoHS compliant product lines.
Utilizing flicker-free UFO high bays and tri-proof tube lighting to eliminate eye strain, prevent workplace accidents, and maintain optimal illumination levels across expansive assembly lines and logistics distribution centers.
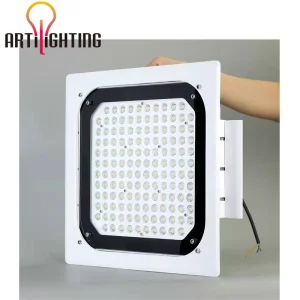
Deploying recessed explosion-proof canopy fixtures with high color rendering index (CRI>80) to ensure crystal-clear visibility, enhanced security, and welcoming customer experiences in 24/7 retail environments.
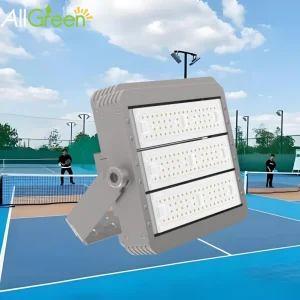
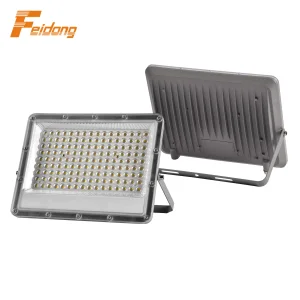
Implementing IP66 modular floodlights and shoebox street lighting designed to withstand heavy wind loads, torrential rains, and thermal fluctuations in municipal and sporting complexes worldwide.
We combine state-of-the-art automated manufacturing facilities in Shanghai with rigorous R&D capabilities. Our fixtures feature customizable wattage, CCT selection, advanced thermal management, and full international certifications (CE, CB, ENEC, UL) tailored to your brand specifications.
Standard production runs typically range from 15 to 25 days depending on order volume and custom requirements (such as specialized housing colors, branded driver integration, or bespoke optical lenses).
Yes! Many of our industrial high bays, wall lamps, and floodlights integrate seamlessly with radar microwave motion sensors, 0-10V dimming, DALI protocols, and smart IoT daylight harvesting systems to maximize energy savings.
We stand firmly behind our engineering quality by offering a 5-year warranty across our core industrial and commercial LED product lines, supported by responsive technical assistance and global logistics coordination.
 Lume Light